Powder Coating Lines for Mexico's Nearshoring Wave: Cabinet Frames and Enclosures
Mexico keeps adding industrial work, and a lot of it lands in sheet metal shops that build electrical cabinets. Most of those shops start with batch ovens and a manual booth. When orders turn steady, the bottleneck moves to the paint shop. A powder coating line clears that bottleneck only when someone builds it around the parts you actually run. Cabinet frames and enclosures come welded, thin-walled, and full of inside corners, so they behave nothing like the flat panels most line layouts assume.
Why Mexico’s Cabinet Frame Shops Are Adding Capacity Now
The demand side is easy to see. Mexico’s merchandise exports rose 7.4% year on year in August 2025, according to INEGI. Nearshoring keeps pulling electrical and appliance work across the border, and analysts expect a second wave once the USMCA review settles after 2027. MarketsandMarkets values Mexico’s powder coating equipment market at USD 11 million in 2024. It expects USD 13.6 million by 2029, a 3.6% annual growth rate. That figure counts hardware alone, so spending on complete lines runs higher.
What a Powder Coating Line Must Solve on a Welded Frame
A cabinet frame is mostly air. Box sections, gussets, door returns, and mounting rails throw long sight-line shadows. Hang density drops because the parts are awkward, not because the conveyor runs slow. And a frame that looks fully coated on the rack can still fail at a weld seam within a season. So a powder coating line has to answer three questions before anyone quotes a price. How do you hang it? Where do the corners get their coverage? And how do you cure a part that carries more surface area than mass?
The Faraday Cage Problem in Frame Corners
Every internal corner fights the electrostatic field. Powder follows field lines to the nearest grounded surface, so it builds on edges and skips the recess behind them. Finishing crews call this the Faraday cage effect. On cabinet frames it shows up as thin coverage in corners, at the base of gussets, and inside door returns. Lower voltage helps. So does a longer spray distance and a second pass from a different angle. The durable fix lives in the layout, though. Rotate the part between passes and you stop paying for touch-up labour for the next decade. Ignore this detail and the line will always need touch-up stations.
How Hang Density Sets the Real Throughput of a Powder Coating Line
Space frames too tightly and you create two problems at once. First, parts shield each other, so some faces come out thin and fail salt spray later. Second, the oven carries more steel than the burners can heat, so cure drops off at the cold end. Space them too loosely and you waste conveyor time. The workable number comes from part geometry and oven capacity, so test it on a sample batch before you build the powder coating line. A line that coats 60 frames an hour with rework is worse than one that coats 45 with none.
Pretreatment and Curing Choices for Mexican Plants
Outdoor enclosure work usually starts here. Zinc phosphating still does the heavy lifting on steel frames. Chromium-free passivation matters more than it did five years ago, because environmental rules tightened on both sides of the border. Buyers increasingly specify ISO 12944 systems. That standard splits durability into four bands. Low means under seven years to first major maintenance. Very high means more than 25 years. Corrosivity class matters as much as the band. A C4 plant near the coast needs a heavier system than a C2 inland plant. ASTM B117 salt spray testing is the usual way to prove the result.
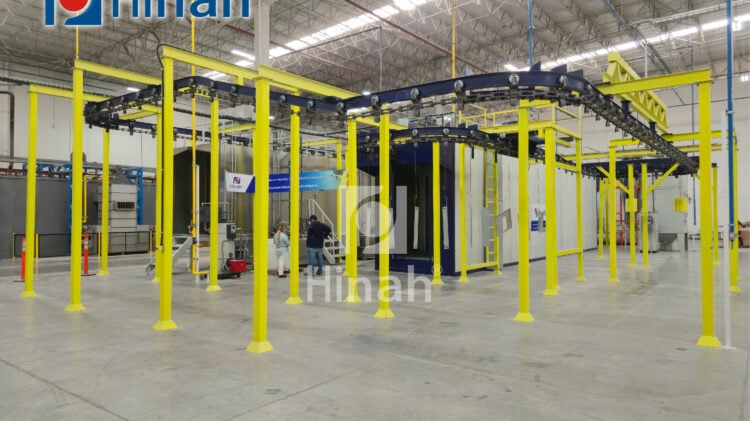
What a Powder Coating Line Project in Mexico Looks Like
A powder coating line project in Mexico has four stages, and each one fails for a predictable reason. Design comes first, and it fails when a supplier designs from a brochure instead of your part list. Fabrication and shipping come next, and they fail when someone sizes pretreatment tanks before testing the water. Installation follows, and it fails when the plant keeps full production running next to an open oven. Commissioning closes the project, and it fails when extra parts arrive that nobody weighed in advance.
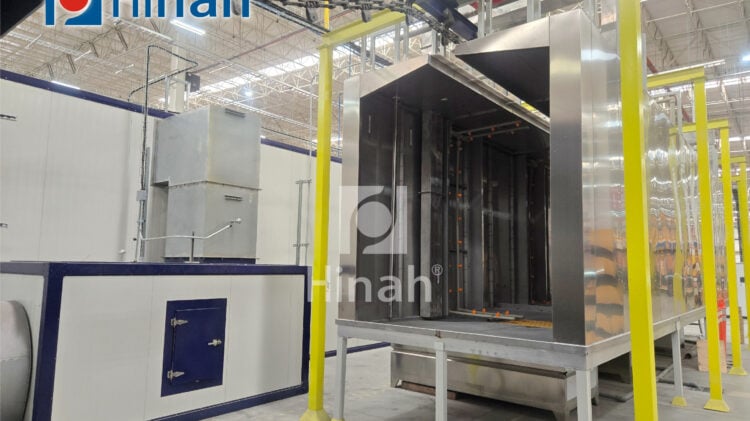
Mistakes That Cost Cabinet Frame Makers Money
Before you sign off on the line, watch for three recurring mistakes. Teams buy on price per conveyor metre and ignore hang density. They skip the sample run, then discover corner coverage problems after installation. They treat powder recovery as a maintenance item rather than a design choice, which lifts cost per part for years.
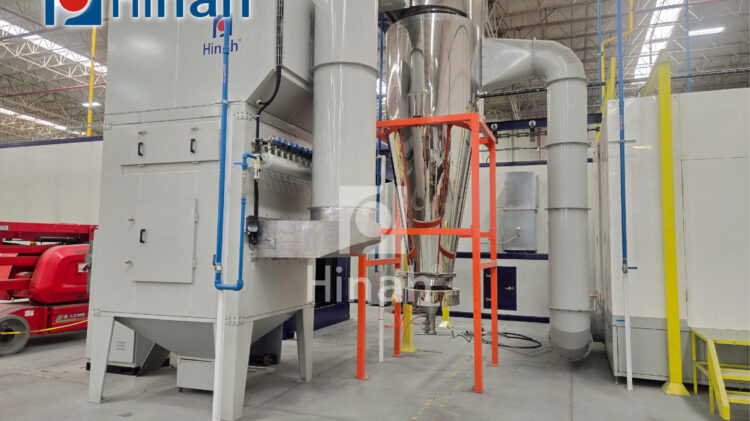
None of this counts as exotic engineering. It is the difference between a powder coating line that fits your part mix and one that fits a supplier’s template. If you are quoting a frame or enclosure line for a Mexican plant, start with the part list, the hang plan, and the corrosion class. Everything else follows.